
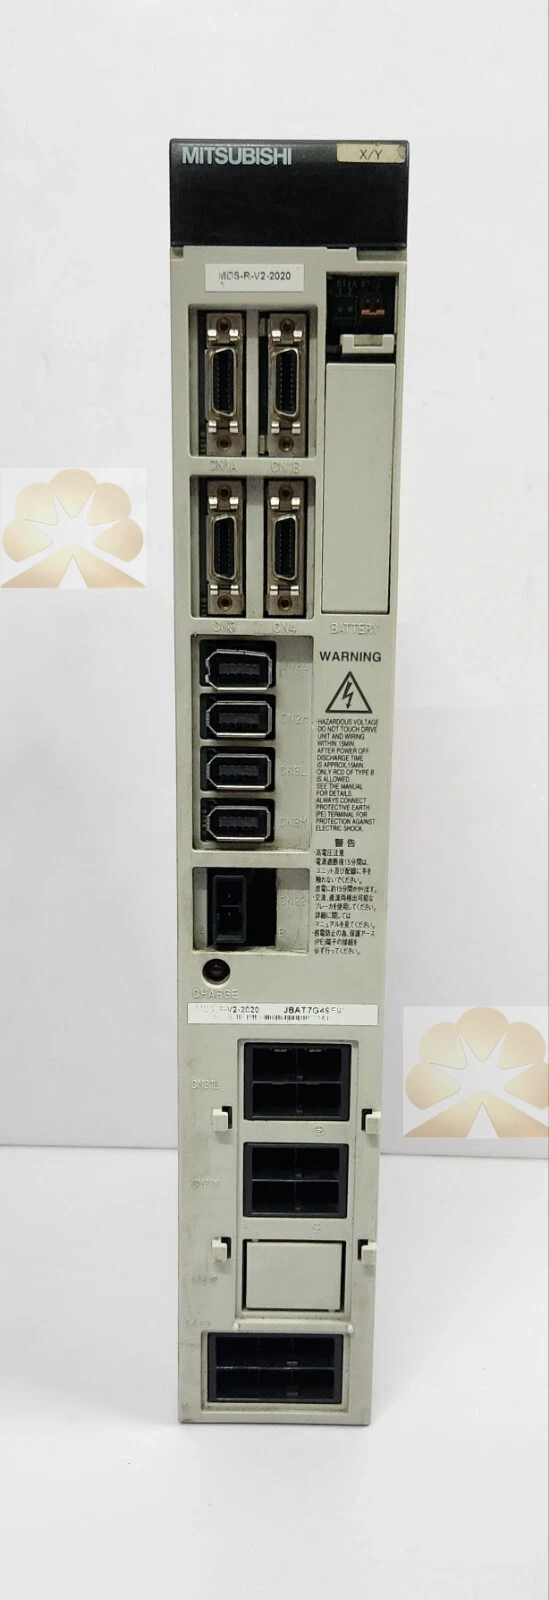
Description
MITSUBISHI MDS-R-V2-2020
Overview
MITSUBISHI MDS-R-V2-2020 is a dual-axis servo drive unit for the Mitsubishi MELDAS MDS-R CNC control system. The suffix V2 means two servo axes integrated within one drive package, and 2020 represents the rated capacity for each axis. This legacy CNC servo amplifier is widely supplied as exchange spare for old machining centers, lathes, grinders and special machine tool cabinet overhaul and axis replacement.
Features
MITSUBISHI MDS-R-V2-2020 integrates two independent servo control channels inside a single compact housing, sharing the common DC bus power from the MDS-R power supply unit. It adopts high-speed optical fiber communication interface to exchange position commands, feedback data and alarm information with the MELDAS CNC controller, supporting high-precision closed-loop position, speed and torque control for feed axes. MITSUBISHI MDS-R-V2-2020 supports incremental encoder feedback for Mitsubishi HF series servo motors. It carries built-in overcurrent, overvoltage, undervoltage, overload, overheat and encoder disconnection protection circuits. Front panel LED indicators display power, ready, alarm and communication status for fast on-site troubleshooting. Fault codes and alarm history can be read via the CNC operator panel or Mitsubishi maintenance software. It supports dynamic brake function for rapid motor stopping during emergency stop and power failure conditions. It complies with CE and EMC standards for CNC cabinet installation.
Specs
MITSUBISHI MDS-R-V2-2020 Platform: MELDAS MDS-R CNC servo system. Type: dual-axis servo drive unit (V2 = 2 axes). Capacity: 2.0kW per axis. Communication: fiber optic link to CNC controller. Feedback: incremental encoder. Power supply: DC bus from MDS-R power supply module. Mounting: installation inside CNC electrical cabinet, paired with matching power supply and motor. This is a dual-axis servo amplifier, not a spindle drive or CNC main controller. MITSUBISHI MDS-R-V2-2020 is widely supplied as service replacement spare for X/Y feed axis control failure on legacy machine tools.
Principle
MITSUBISHI MDS-R-V2-2020 receives position command pulses from the CNC system over fiber communication. Each channel executes independent PID closed-loop calculation, outputs PWM signals to drive the corresponding servo motor. The encoder signal from the motor feeds back actual position and speed back to the drive for deviation correction. If overcurrent, overheat, encoder loss or DC bus fault is detected, the drive immediately cuts off the PWM output, activates dynamic brake and sends an alarm message to the CNC host, which then stops the machine movement and records the fault event.
Applications
MITSUBISHI MDS-R-V2-2020 is deployed for vertical machining centers, CNC lathes, surface grinders and automation special machines equipped with MELDAS MDS-R control. It is selected for spare inventory and cabinet retrofit projects for existing MDS-R dual-axis servo control systems. Modern replacement options are Mitsubishi MDS-D2 and MDS-E series servo drives.
Get a Quote